Curated commercial furnishing solutions engineered for heavy-duty utilization in hotel lounges, residential complexes, and luxury dining spaces.
A globally recognized partner in contract manufacturing, precision cabinetry engineering, and bespoke commercial interior solutions.
Guangdong Ambrose Home Co., Ltd. is located in Foshan City, Guangdong Province, China, a globally recognized hub for furniture manufacturing and home furnishing innovation. The company is dedicated to the research and development, design, production, sales, and customization of high-quality solid wood furniture, upholstered furniture, and mattresses, providing comprehensive one-stop home furnishing solutions for global customers.
We specialize in whole-house customization services, covering living rooms, dining rooms, bedrooms, studies, and other residential spaces. Our goal is to deliver integrated home solutions that combine aesthetics, comfort, and functionality, tailored to the diverse needs of modern lifestyles. Under our strict Company Positioning, we focus on premium material selection, refined craftsmanship, and human-centered design. We are committed to providing every customer with high-quality products and warm, professional services, carefully tailored to different lifestyle needs and market segments.
By blending cultural heritage with modern design trends, we integrate innovative concepts into every product. Our design philosophy emphasizes humanization, practicality, and contemporary aesthetics, aiming to create a new generation of home furnishing styles that lead industry trends and enhance living experiences.
Analyzing key commercial parameters, material structural integrity, and procurement drivers for developers, procurement heads, and hospitality buyers.
In high-traffic environments like hotels, fine dining establishments, and banquets, cabinetry must withstand constant door operations, damp plate contact, and high load forces. We prioritize structural framing using kiln-dried solid ash, American walnut, and reinforced metal subframes.
Modern commercial dining server cabinets are no longer simple storage units. They house integrated wine cellars, hot/cold plate drawer setups, integrated cutlery organizers, and hidden electrical channels. We design with precise millimeter tolerances for standard kitchen appliance integration.
Major corporate buyers and real estate developers require low-VOC, CARB Phase II, and FSC certifications. We secure lumber from sustainable, managed forests and finish products with eco-friendly water-resistant UV coatings that comply with strict global safety thresholds.
A programmatic, engineering-driven method detailing custom sideboard development from blueprinted drafts to mass floor manufacturing.
Our OEM dining server cabinet pipelines commence with structural CAD model drafts. We design internal cabinetry skeletons to account for shear stress, uniform load distributions, and thermal fluctuations if warmer plates or refrigerators are enclosed. Our engineering teams ensure that hardware selections match or exceed the standard commercial cycle expectations (e.g. over 80,000 door openings).
Server cabinets are prone to hot beverage rings and sauce spills. Guangdong Ambrose Home utilizes multi-layered PU (Polyurethane) coating lines combined with anti-bacterial protection. Our water-resistant and scratch-resistant finishes prevent moisture penetration and preserve the natural texture of the underlying wood grain, minimizing the risk of warping, discoloration, or microbial colonization in commercial dining sectors.
A step-by-step breakdown of Ambrose Home's rigorous production stages, demonstrating true manufacturing expertise and quality control.
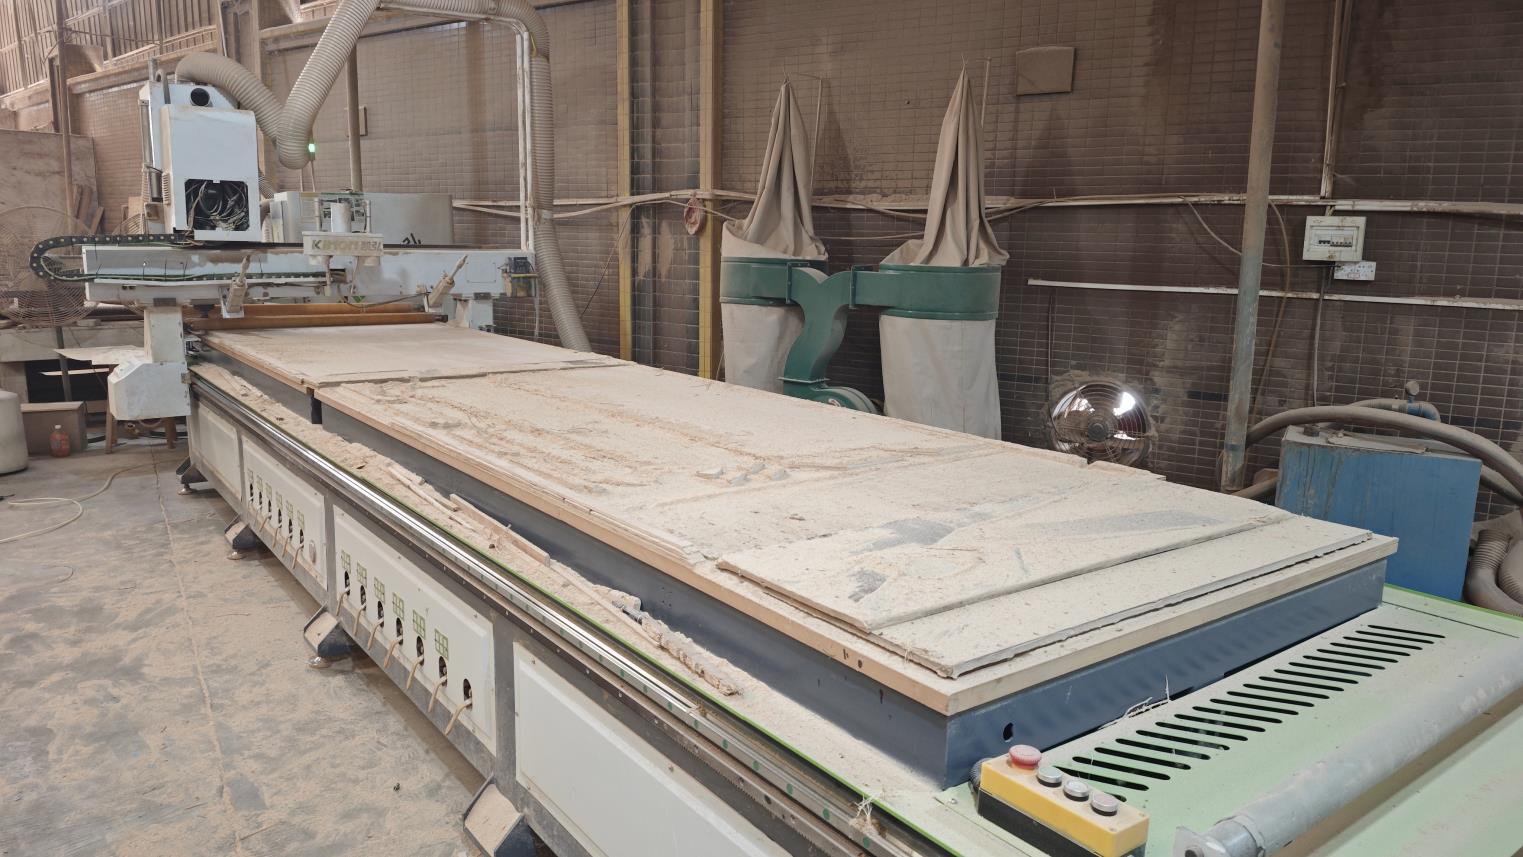
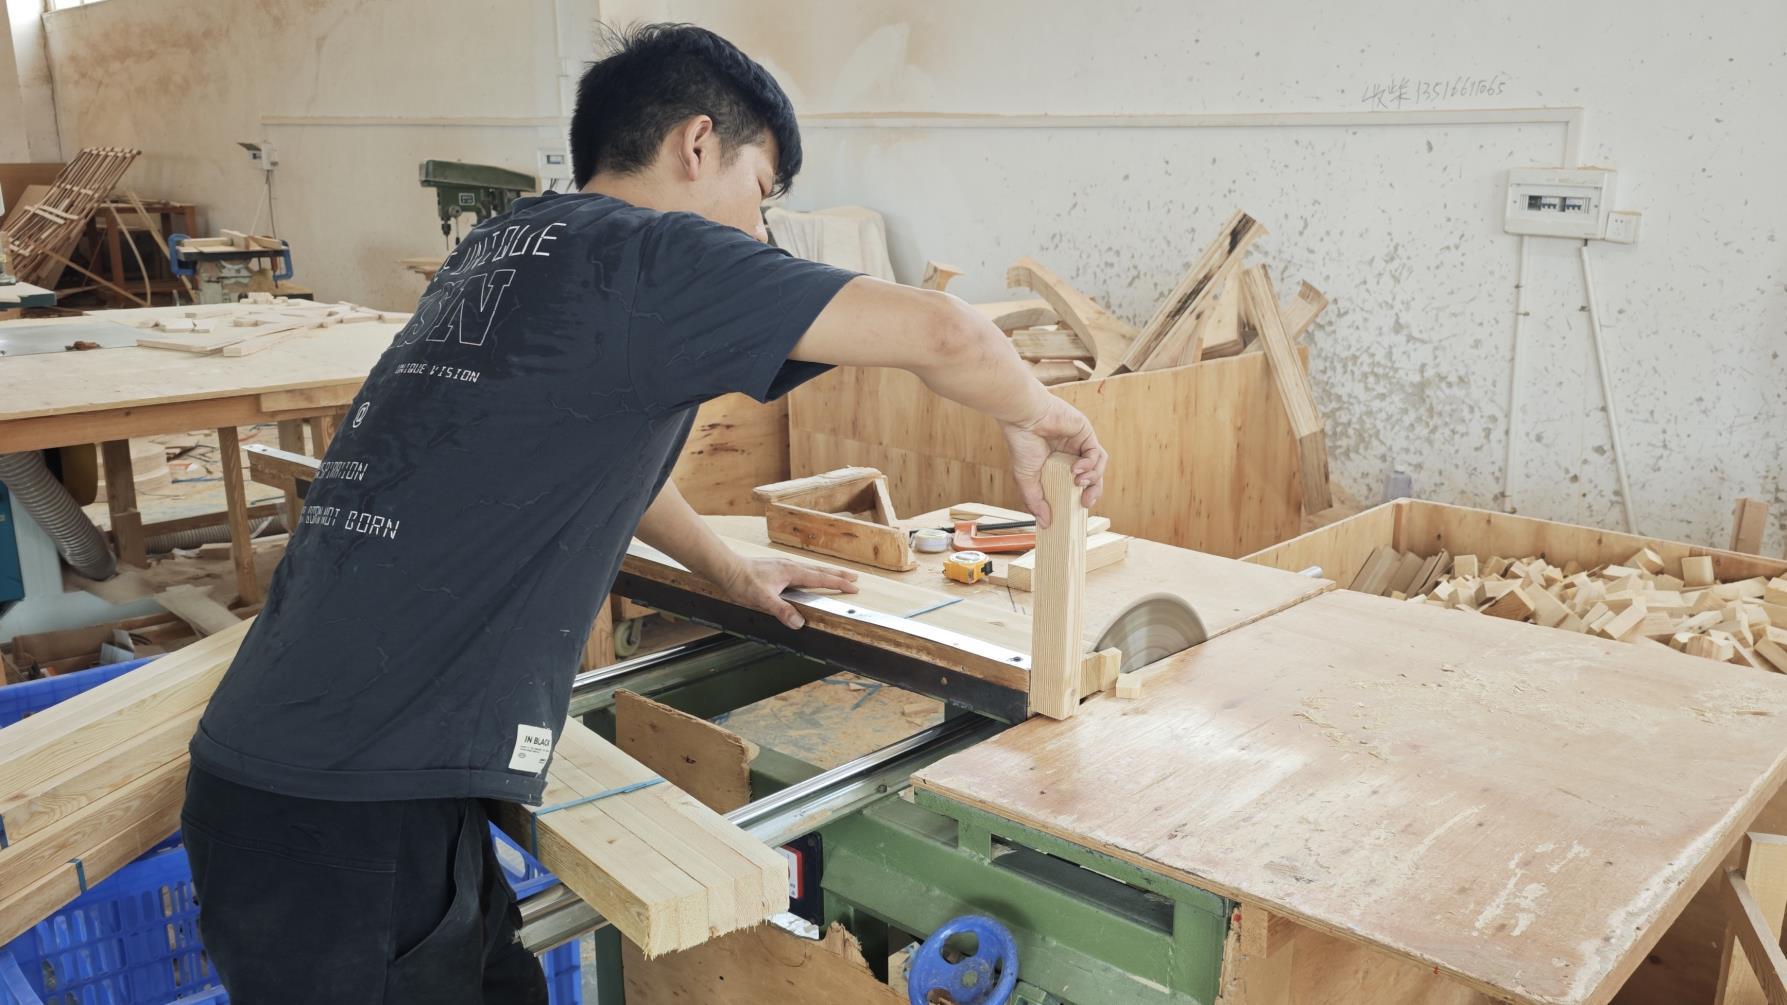
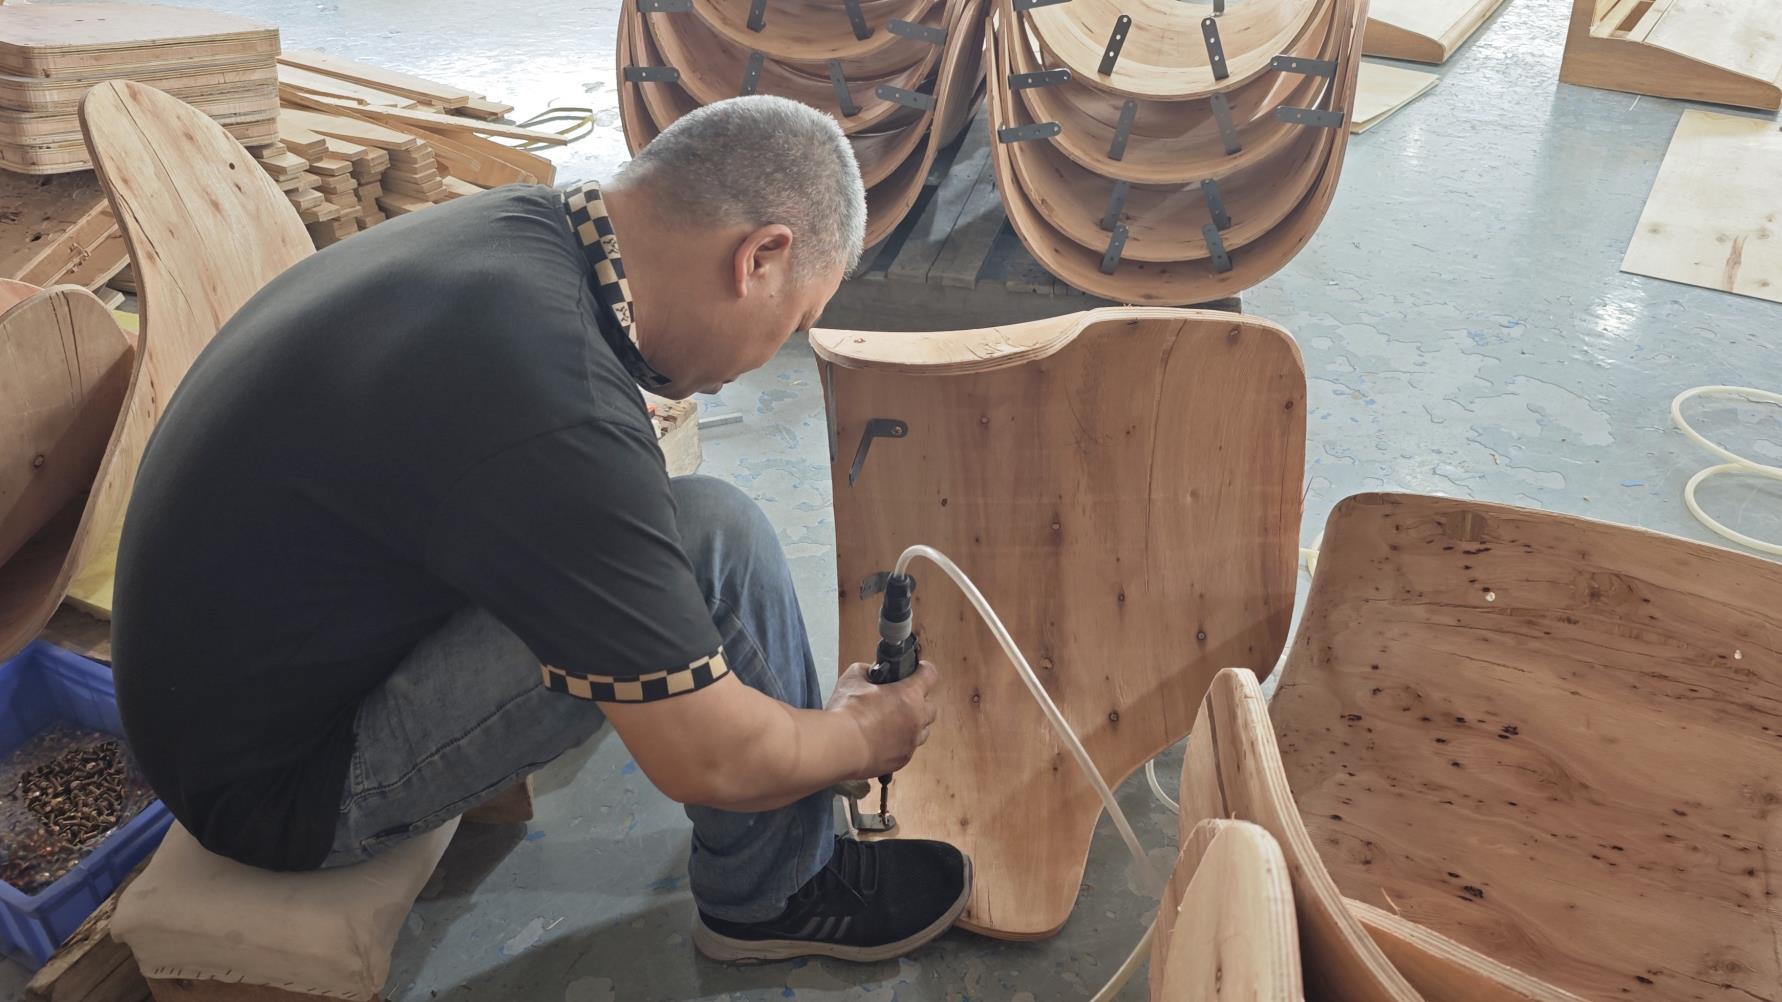
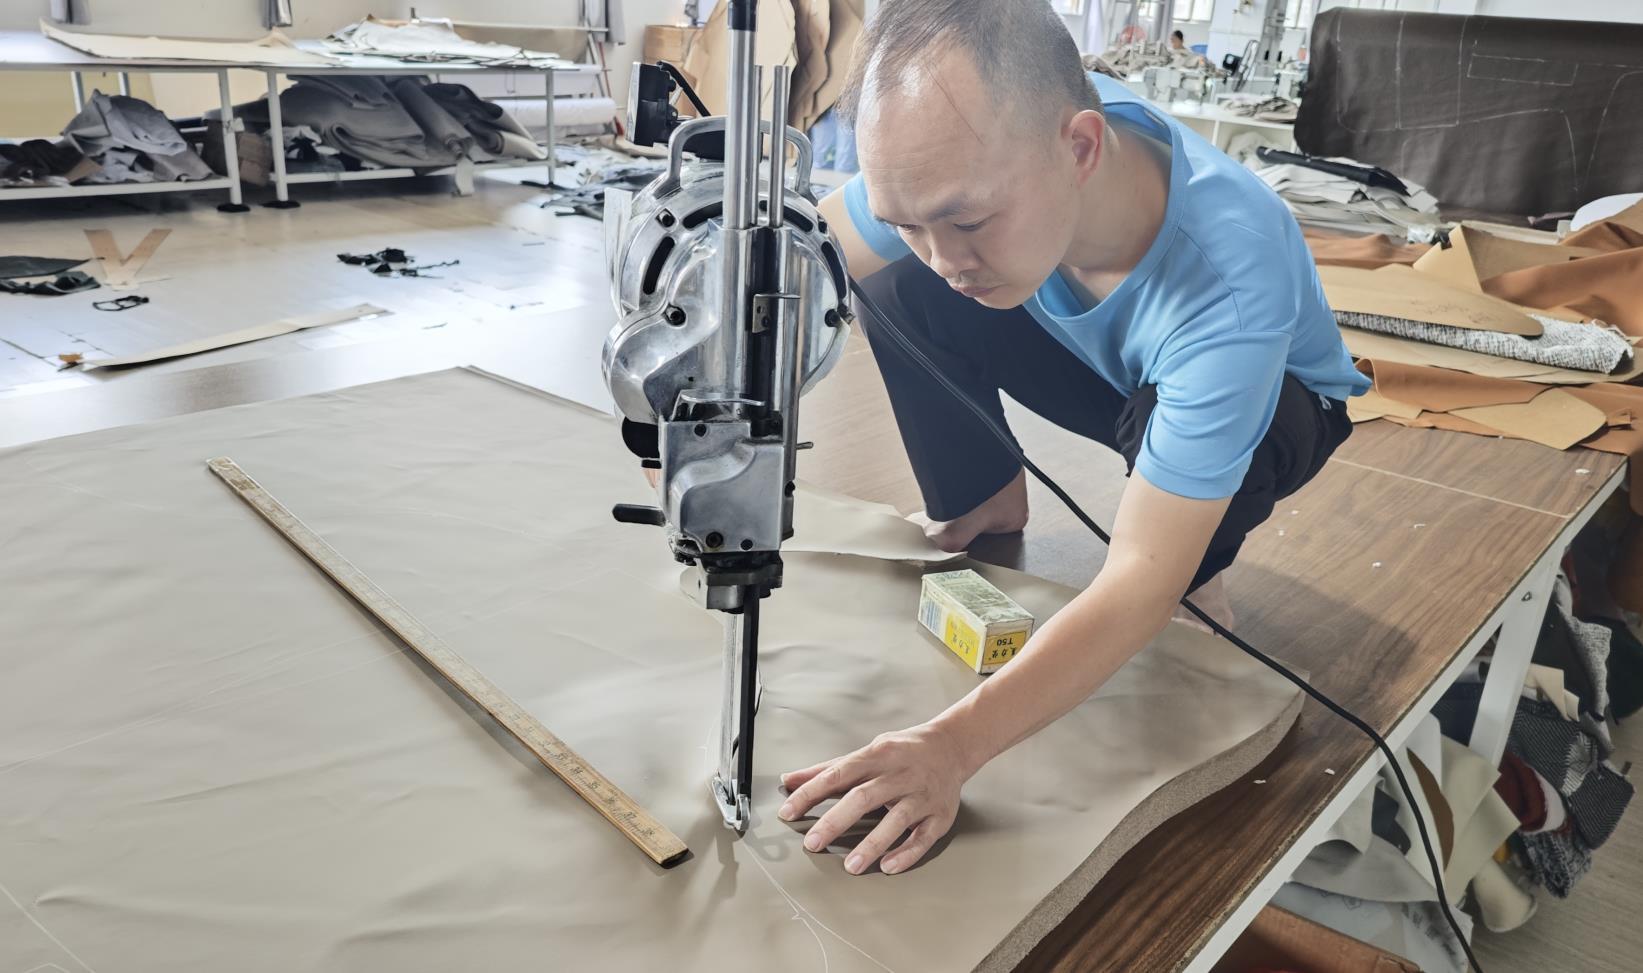
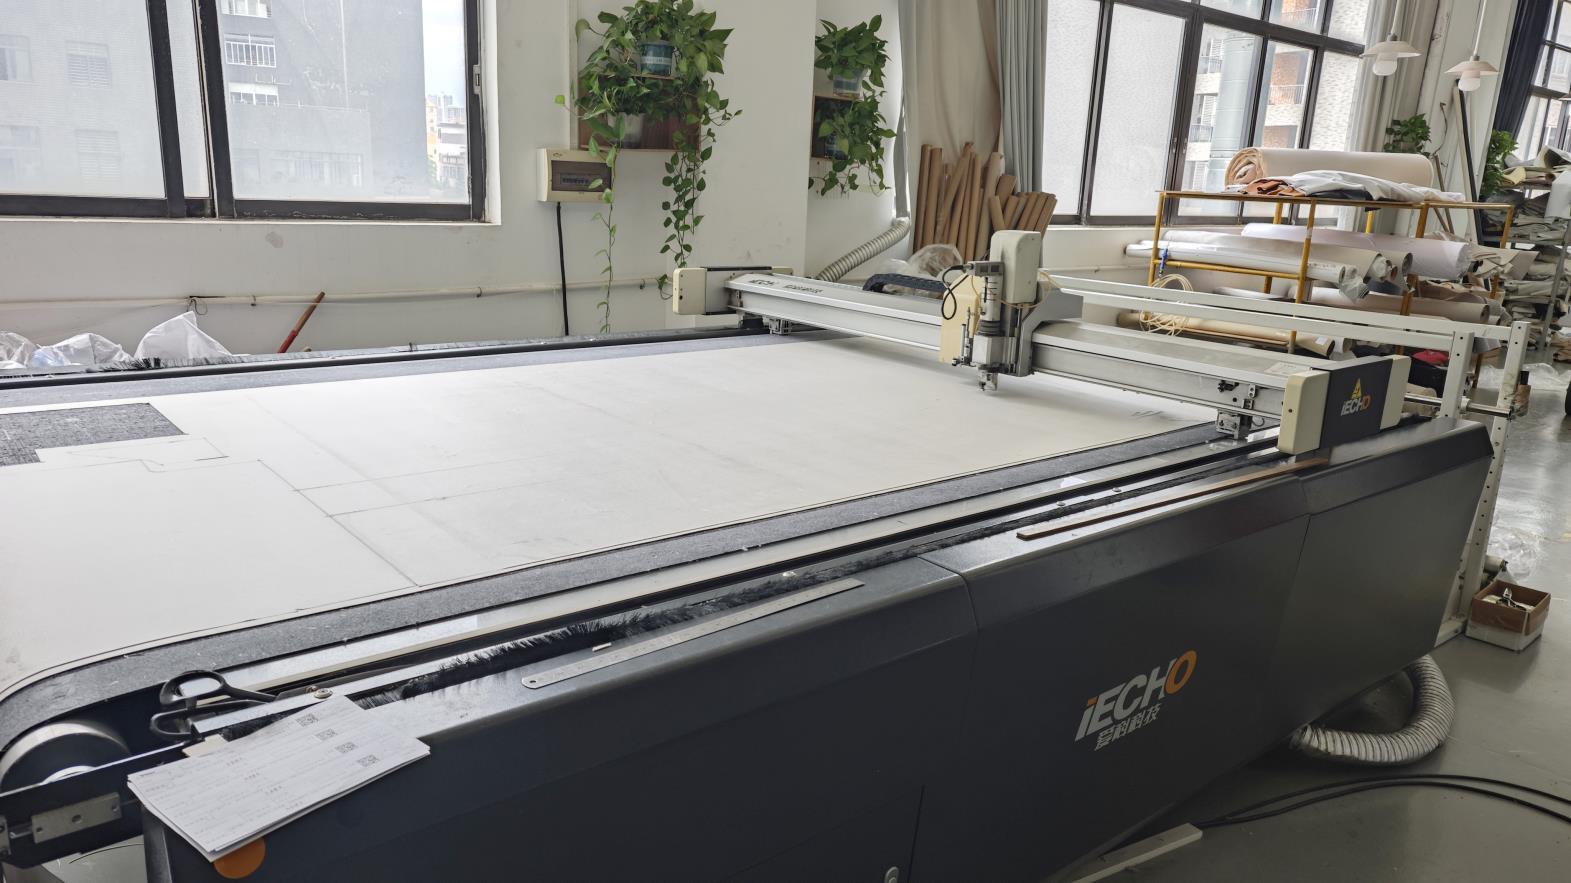
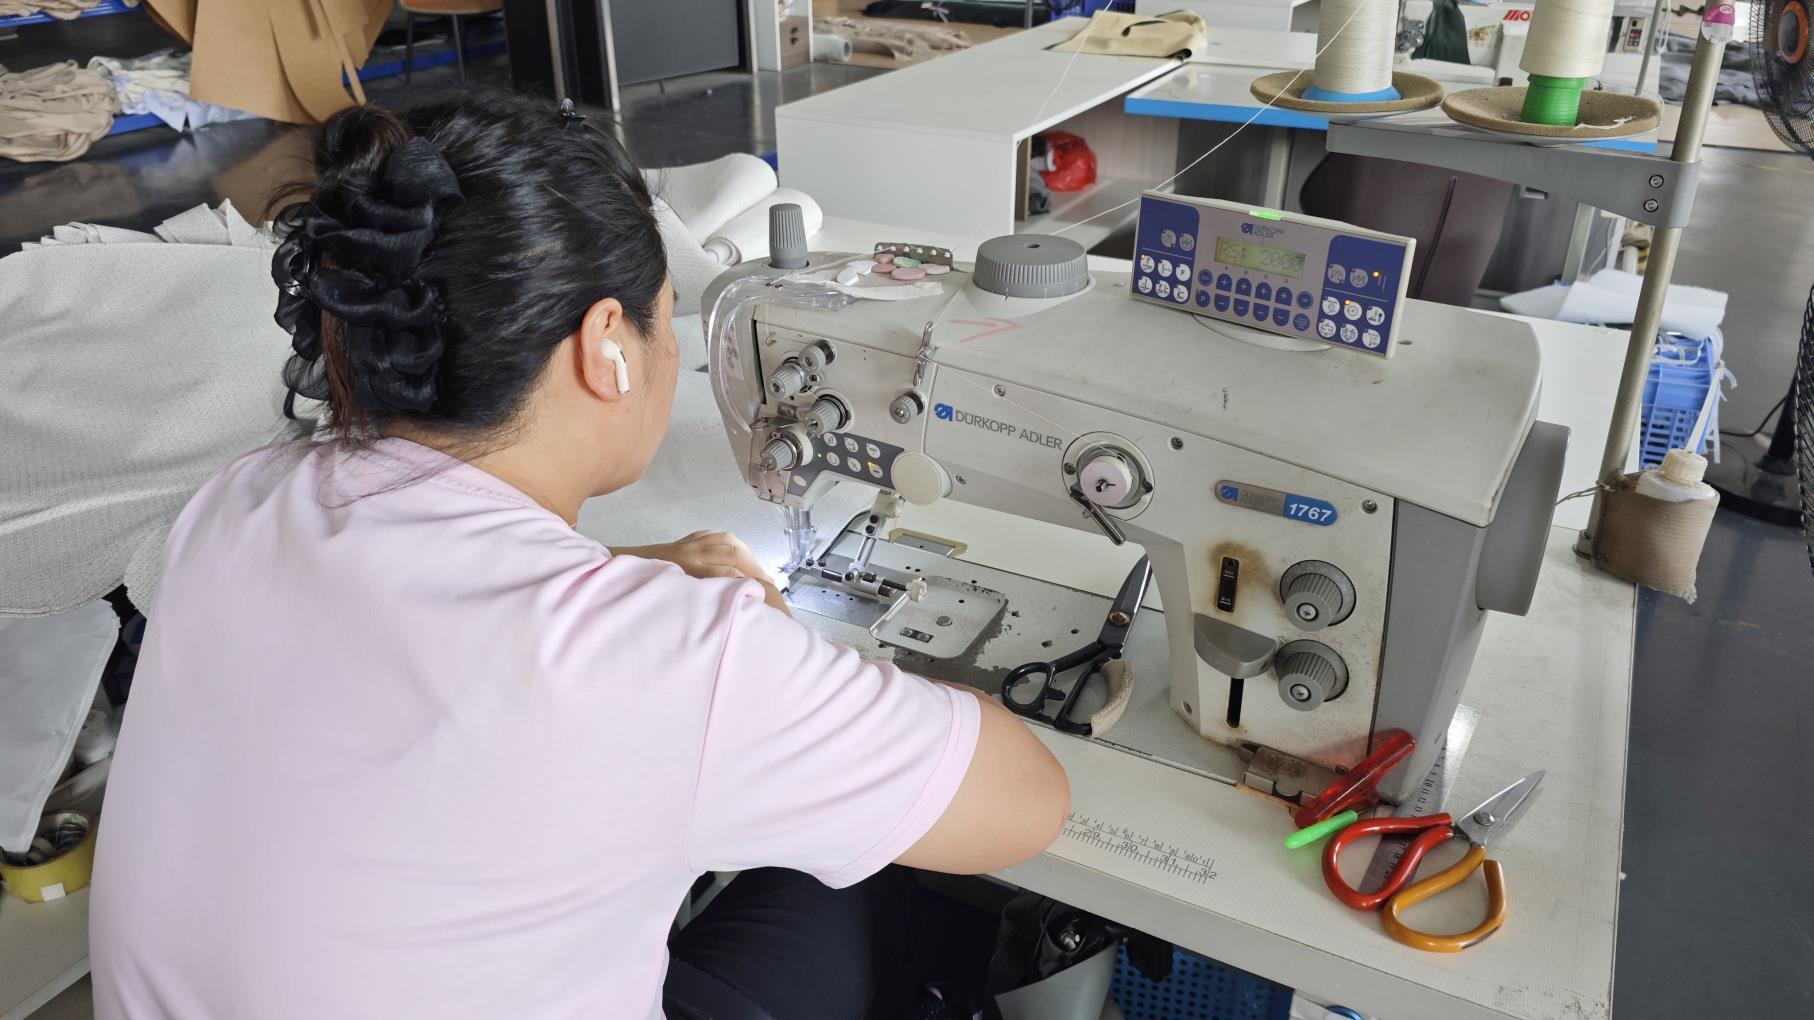
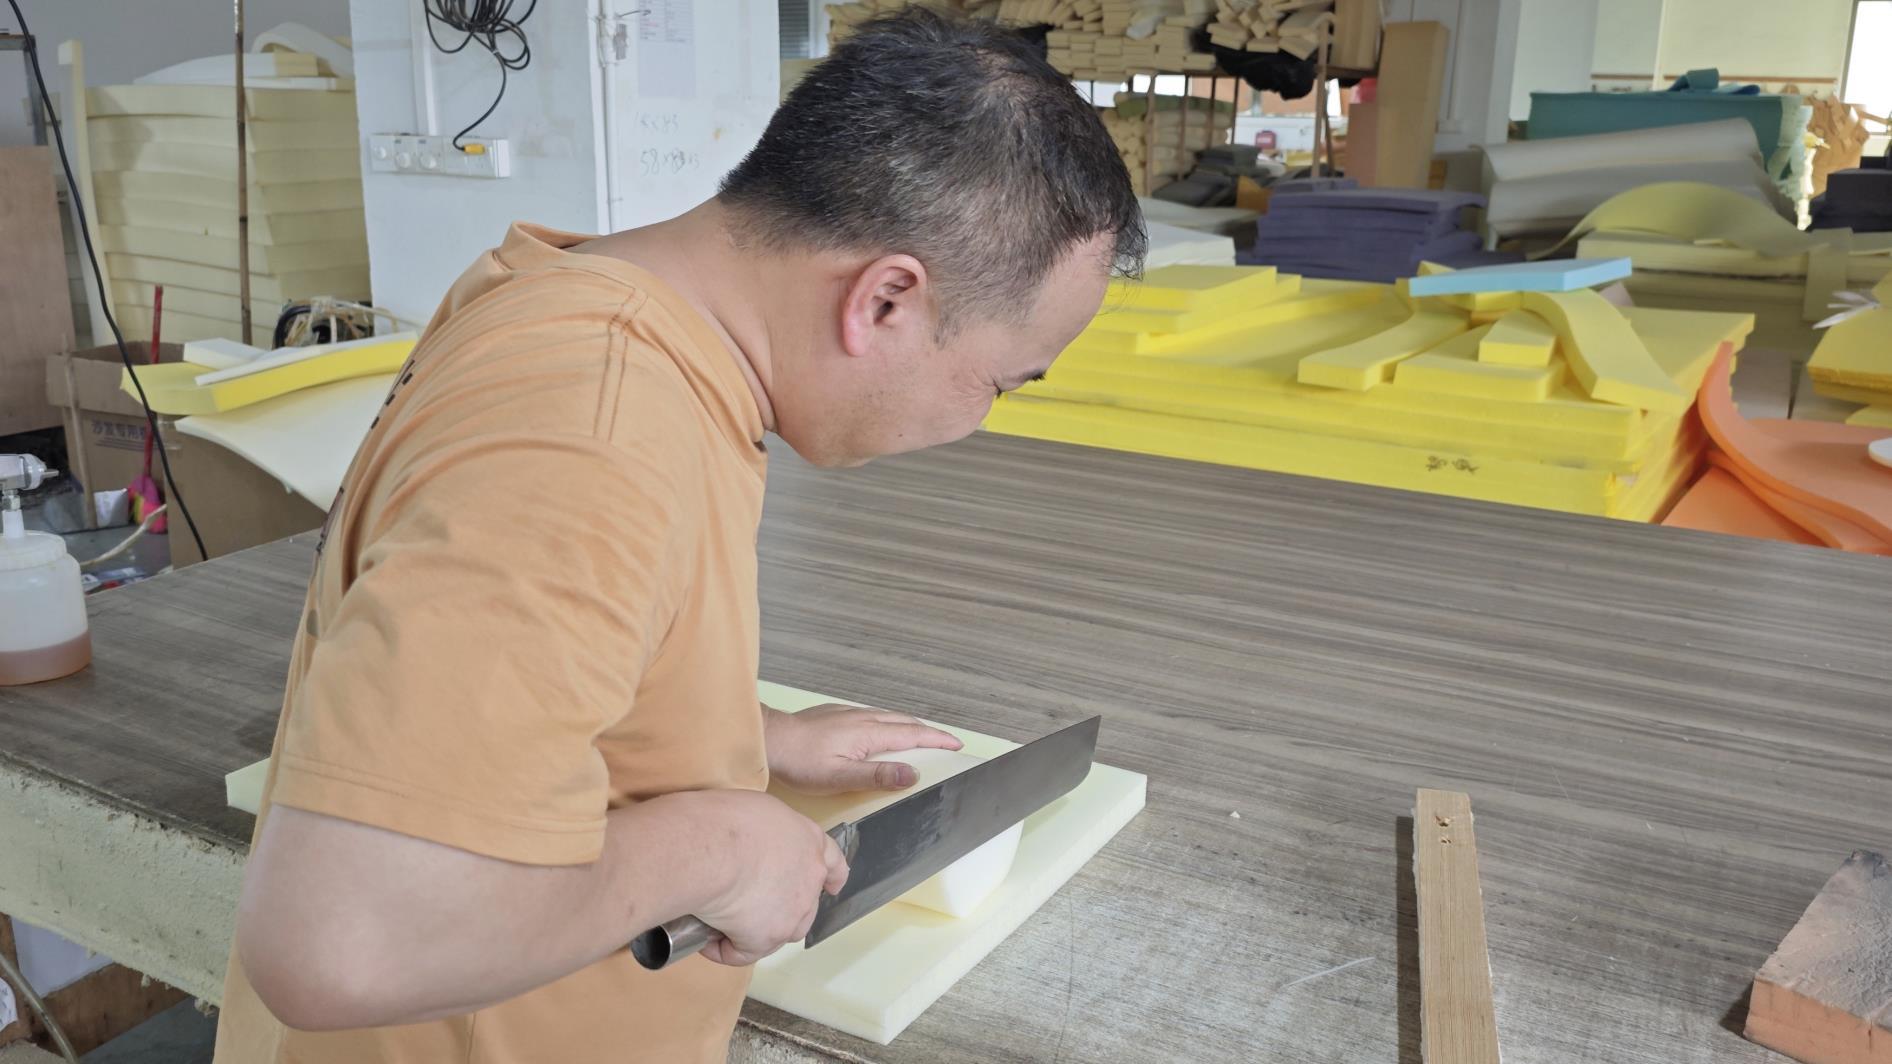
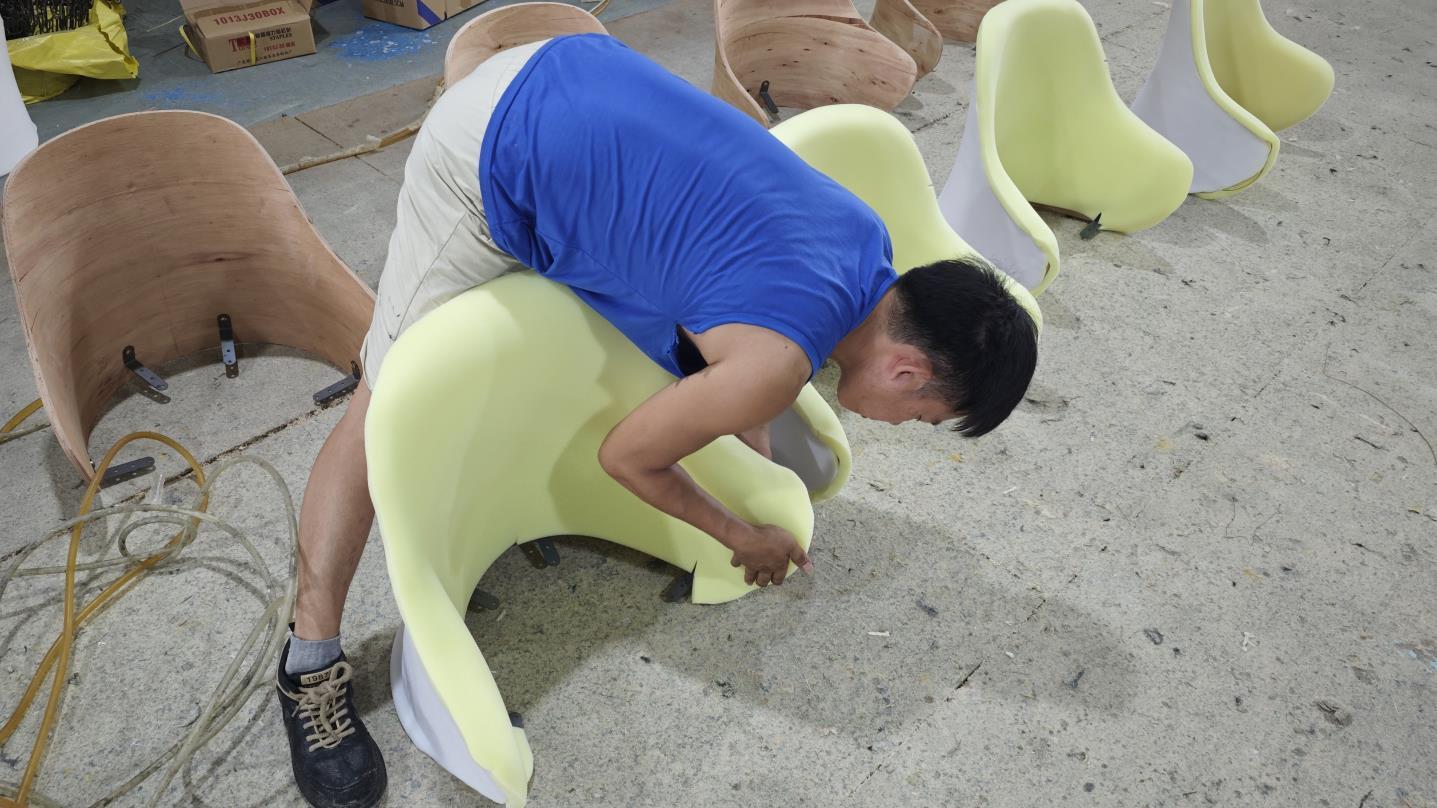
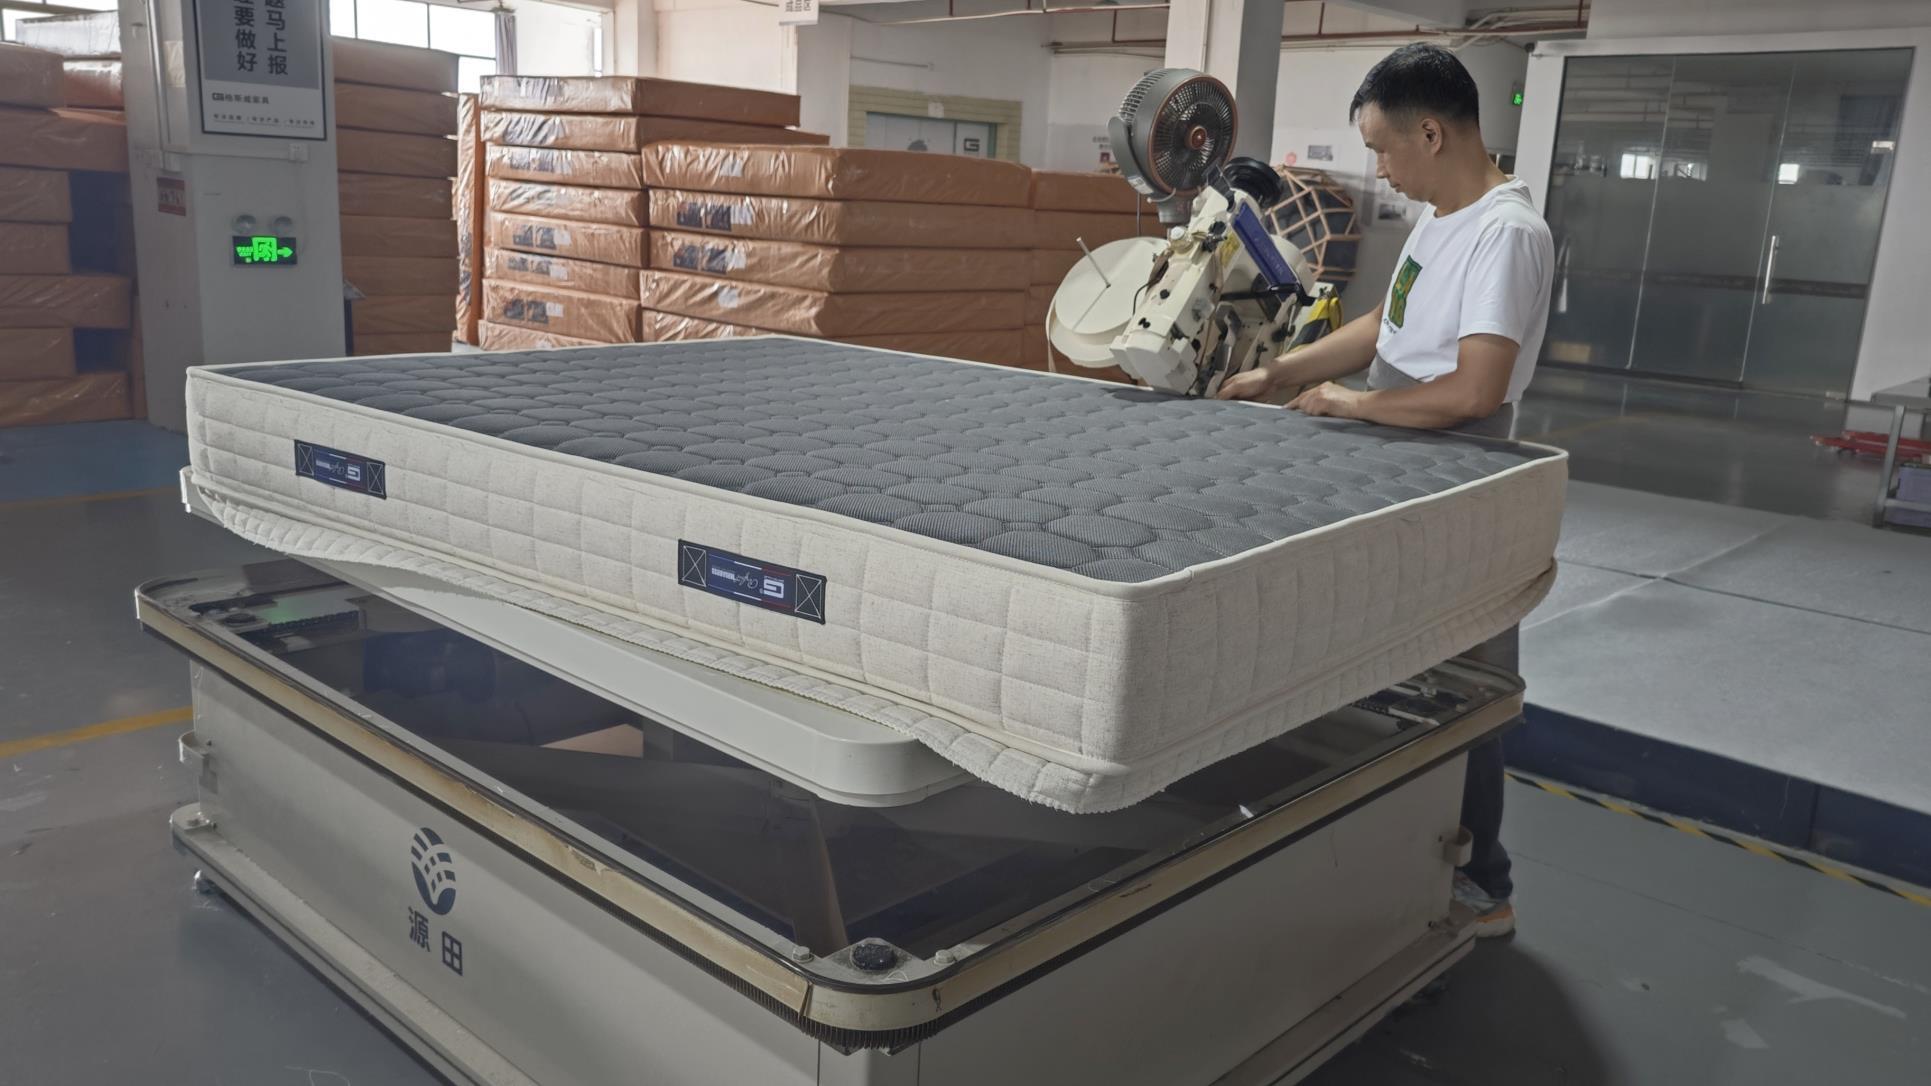
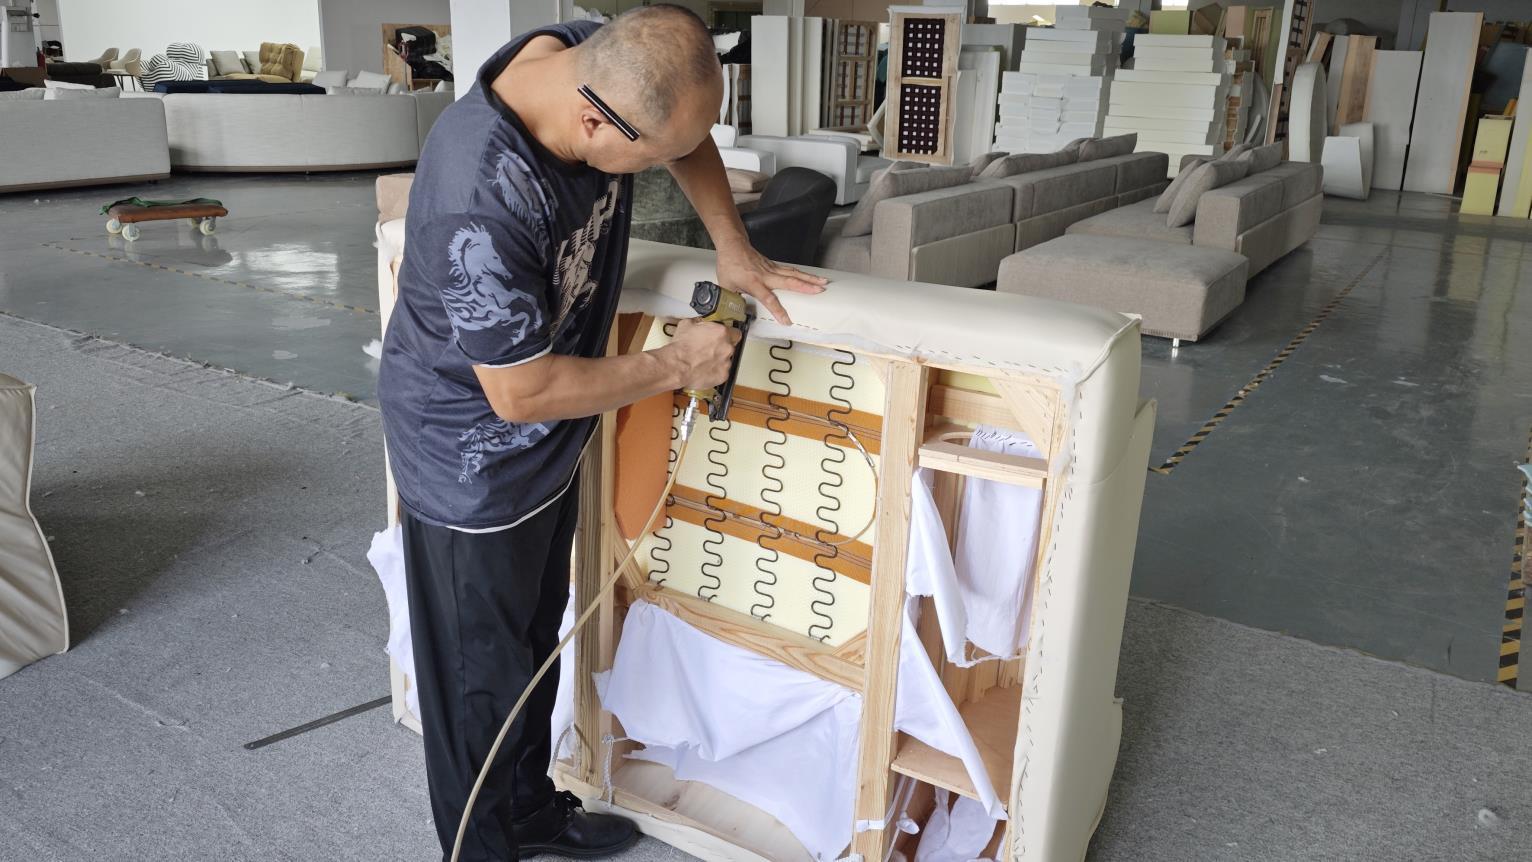
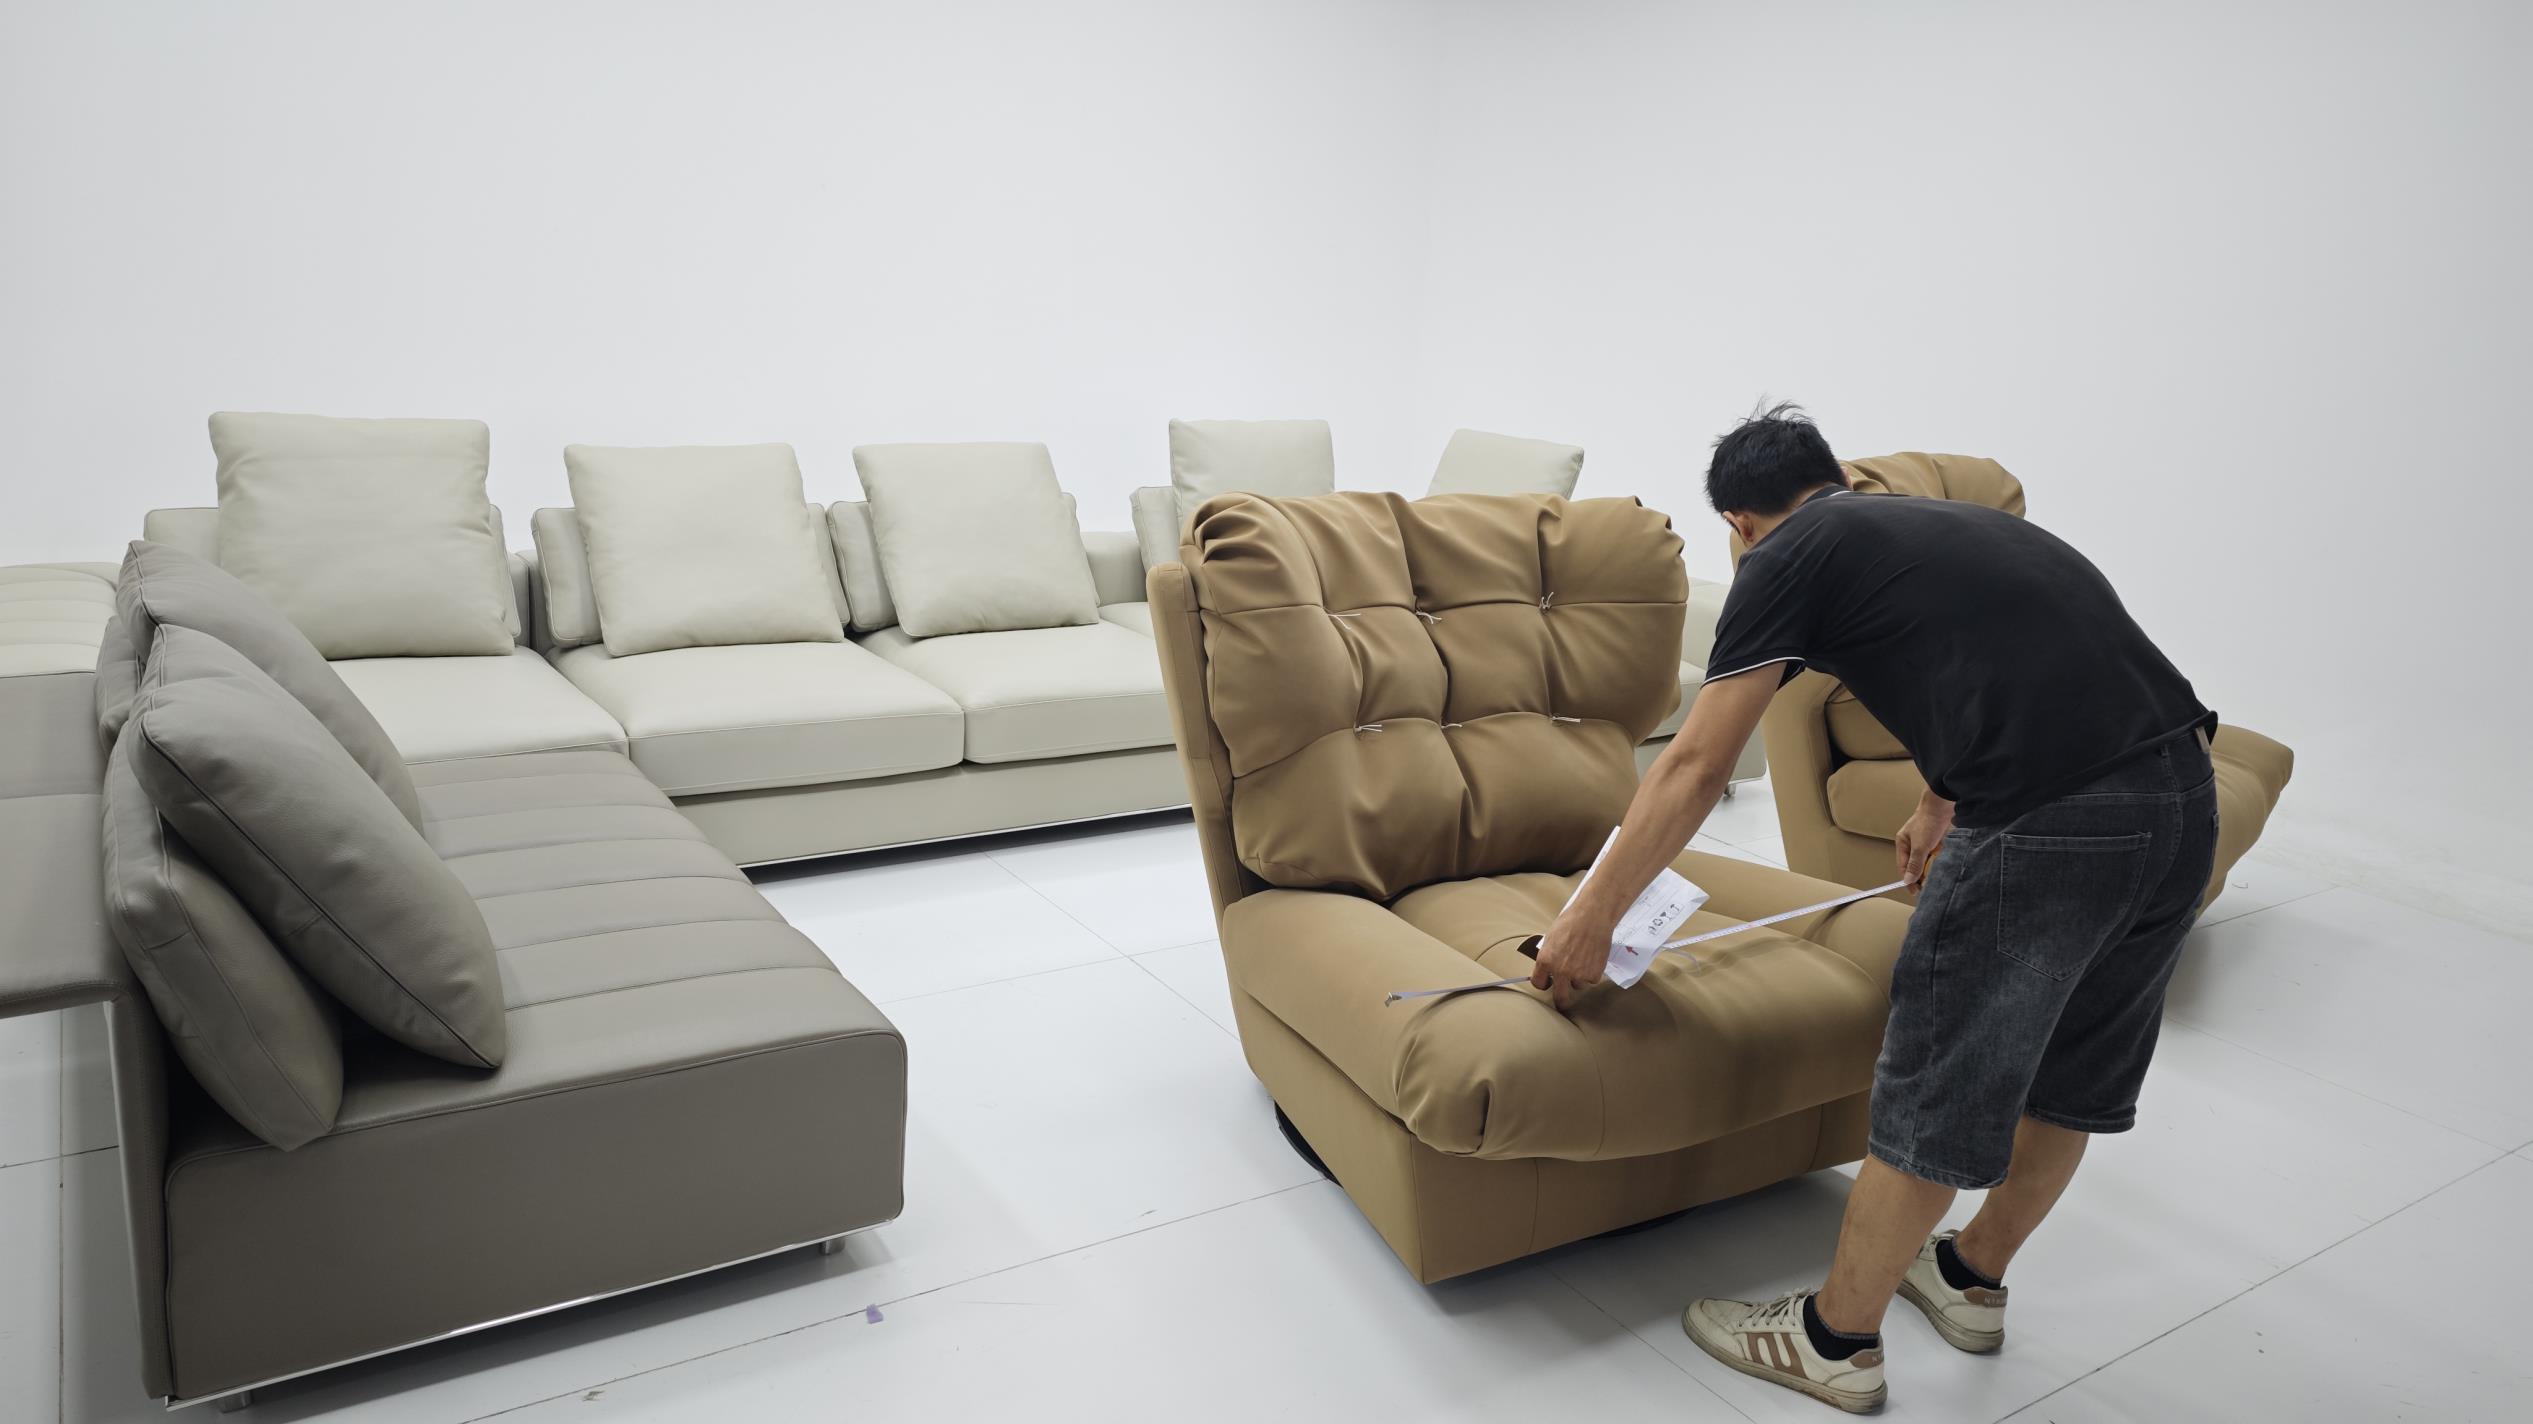
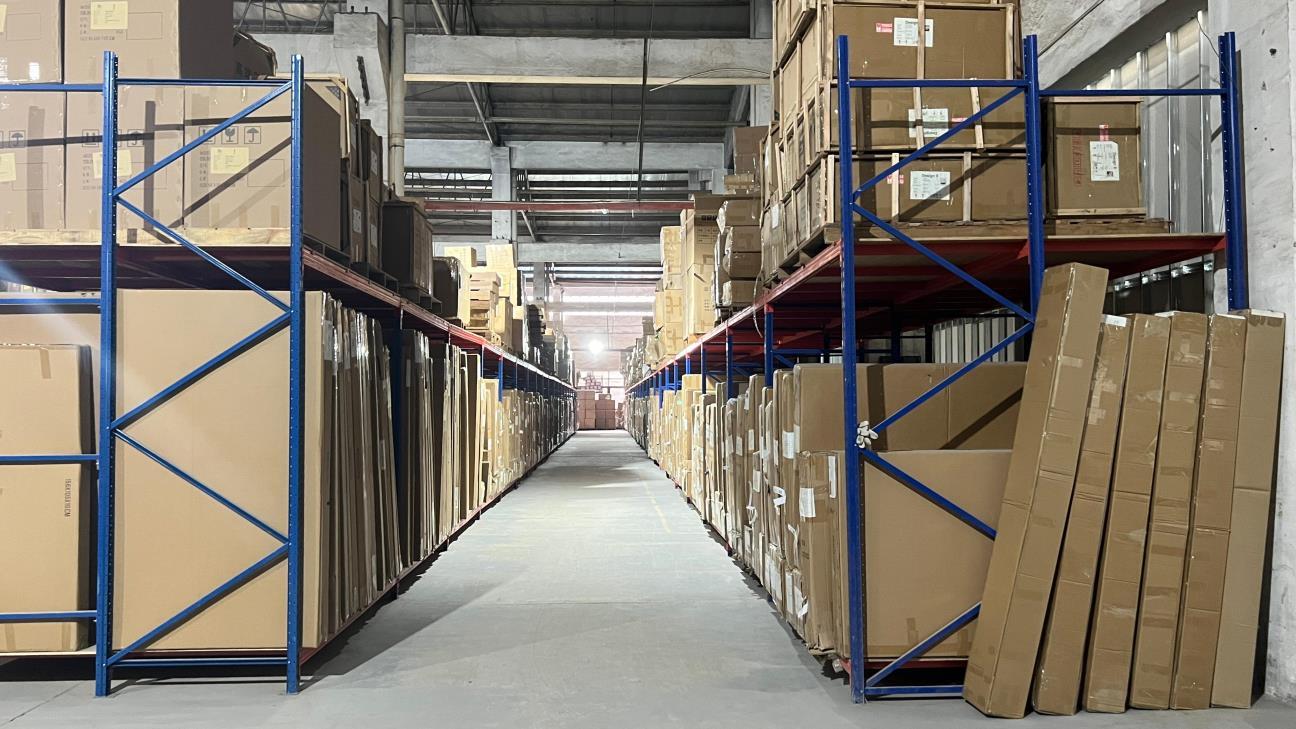
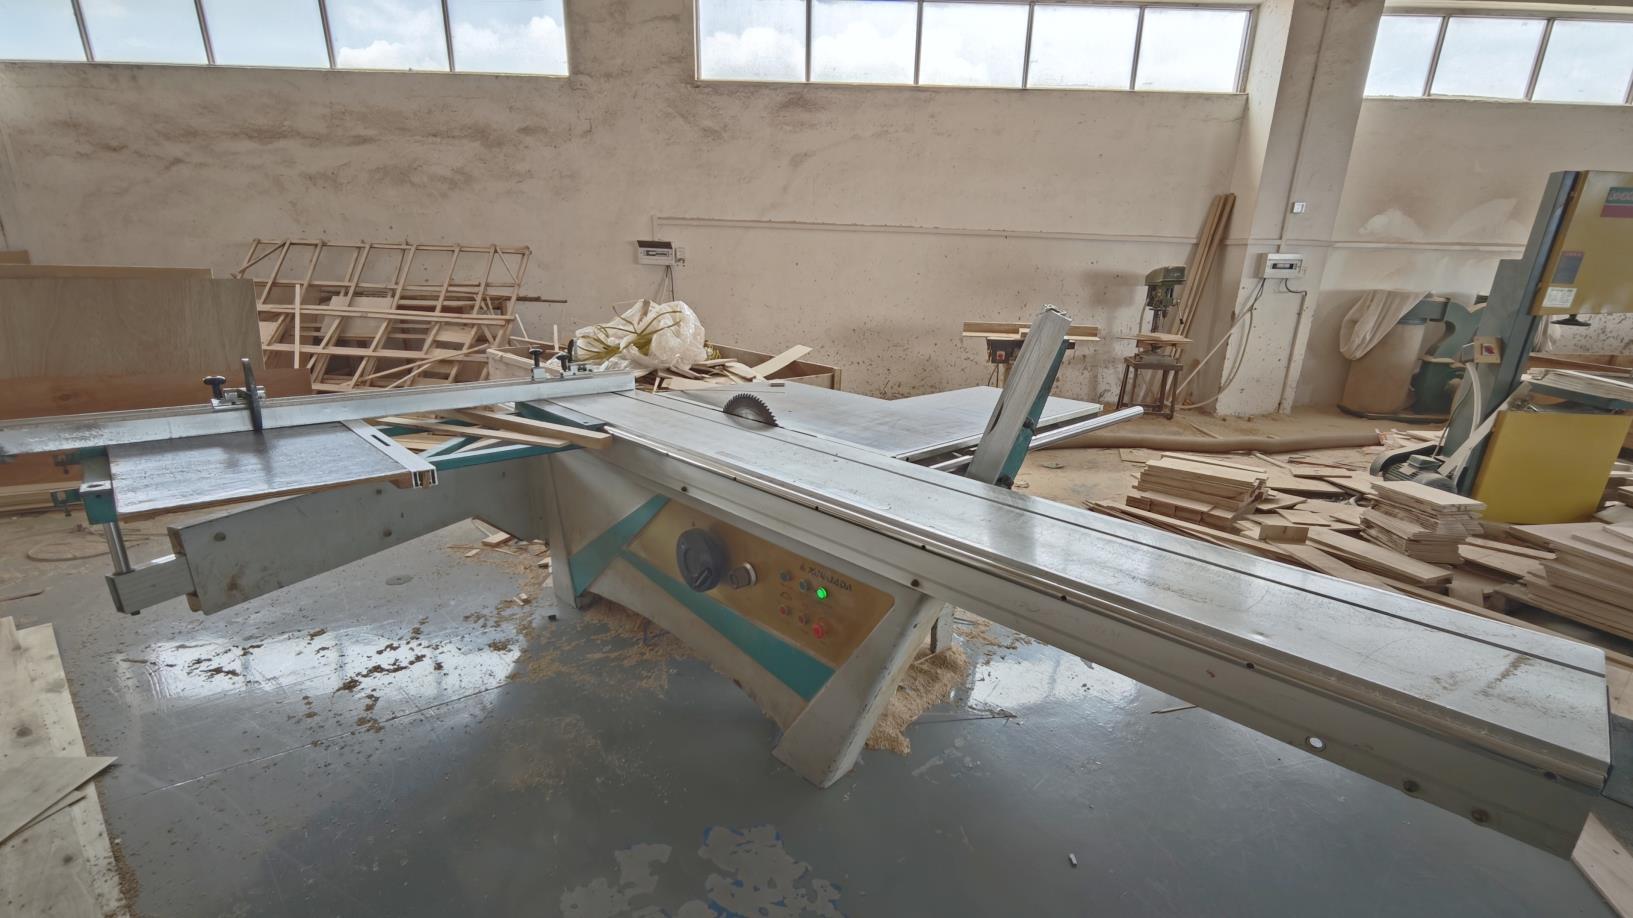
Pioneering intelligent integration, mechanical reliability, and modular sustainability in commercial cabinetry environments.
Integrating compact cooling chambers and heating elements within dining credenzas. In corporate and lounge environments, this feature keeps dishes at serving temperatures while storing chilled wine in dedicated climate-controlled compartments.
Future designs incorporate flush wireless inductive chargers on the stone or timber countertops, and USB-C port panels disguised in magnetic pop-out recesses, providing mobile charging options for modern guests.
Switching components to modular assembly layouts, where side panels, front doors, drawer faces, and runner systems are separately replaceable. This extends the service life of cabinets by allowing simple repairs rather than full unit replacement.
Mitigating cross-border freight risks, ensuring regulatory clearance, and adhering to strict international furniture safety regulations.
Shipping custom furniture worldwide requires strict compliance with international mechanical and environmental guidelines. Our products undergo rigorous testing, ensuring stability, structural load limits, and tipover prevention under ANSI/BIFMA X5.5 (Desk and Table Products - Tests) and EN 14749 (Domestic and kitchen storage units safety requirements).
For chemical and emissions compliance, our factory utilizes low-emission raw materials and finishes that meet EPA TSCA Title VI (Formaldehyde Emissions Standards for Composite Wood) and California Air Resources Board (CARB) Phase II requirements. Additionally, our solid timbers can be FSC certified upon request, verifying that the lumber is sourced from sustainably managed forests.
To prevent shipping damage, all items are wrapped in multi-layered polyethylene foam, packed in high-density double-wall corrugated cartons, and secured with corner protectors. For heavy custom sideboards, we build bespoke reinforced plywood crates to ensure safe ocean freight and logistics handling.
Answers to critical technical, lead time, and structural questions from buyers and project managers.
For standard custom finishes, our MOQ starts at 20-50 units per design. However, for large commercial hospitality projects, hotel refits, or custom residential developments, we can adjust batch configurations to align with project milestones.
We use certified E0 and E1 grade medium-density fiberboards (MDF) and plywood from verified suppliers. Every material delivery is accompanied by mill testing certificates, and our finished products undergo third-party laboratory chamber tests to ensure chemical compliance.
By default, we utilize high-durability DTC undermount soft-closing runners and 3D-adjustable concealed hinges. Upon client request, we can integrate premium European hardware like Blum or Hettich to match specific project specifications.
CAD design and engineering blueprints are generated within 5-7 working days. Once approved, the physical sample prototype is produced in 15-20 days. Mass production averages 35-45 days, depending on material specifications and order volume.
Yes. We regularly design cabinets with rear ventilation grills, heat-reflective aluminum backing panels, internal cable management ducts, and pre-drilled grommets to safely accommodate compact warming drawers, minibars, or coffee machines.
We utilize drop-tested packaging layouts. Each cabinet is encased in high-density foam, secured with corner protectors, and packed in heavy-duty export cartons. For consolidated shipping (LCL), units are secured in solid wooden crates to protect them from fork-lift damage.
Explore our complete commercial furniture catalog, including seating, tables, and cabinets designed for contemporary hotels, offices, and projects.
 Ambrose Home


